

At a Glance
- 1 Pilot Grade Released
- 0 Leak Failures in Pilot
- 15% Faster Changeover
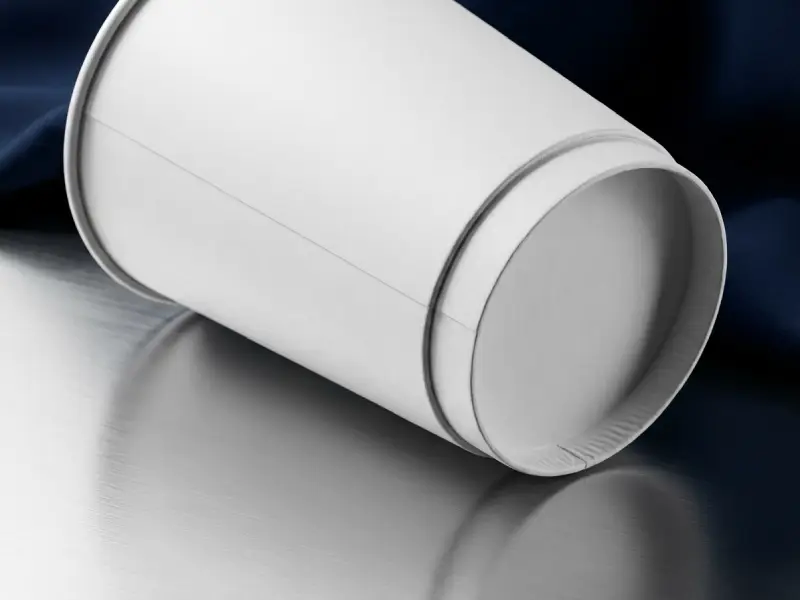
Bottom seal validation on recyclable coated board.
Removing PE film changed both forming behavior and seal performance
The customer needed a recyclable cup structure, but the switch away from conventional film lamination introduced uncertainty at both the side seam and bottom seal.
- Forming teams were concerned about leak resistance during hot-fill use.
- Material changes affected friction and heat profile on existing cup machines.
- Brand owners needed pilot data that repulpability screening and shelf performance could be reviewed on the same qualified structure.
A coordinated coating-and-bonding package rather than a one-part swap
Senda aligned barrier coat behavior, adhesive anchorage, and machine settings so the pilot grade could pass leak screening and the customer internal repulpability checklist on the qualified structure.
Products Used:
- Repulpable Barrier Coating
Delivers liquid holdout while supporting fiber recovery.
- Cup Forming Adhesive System
Stable bond formation on coated cup stock at commercial speed.
The key was treating the cup as a system. Instead of asking the adhesive alone to compensate for every material change, the project optimized coating chemistry, bond geometry, and forming conditions together.
Qualification path
Barrier and bond screening
Coating holdout, side-seam green strength, and bottom-seal behavior were screened together on the target aqueous board grade.
Machine-side forming trial
Cup lines ran at commercial speed with friction, heat, and changeover tracked against the prior PE-laminated reference.
Hot-fill and recyclability review
Pilot cups moved through leak testing and the customer recyclability checklist before release approval.
Pilot outcome
Pilot outcome
Internal recyclability and forming checklist cleared on the qualified cup structure before scale-up review.
Across the final hot-fill and hold tests in the pilot run.
Operators reached stable settings faster on subsequent SKU runs.
Related resources
- FDA 175.105 vs 176.170 vs FCN: Which Food-Contact Route Fits Your Packaging?
Documentation-path guide for indirect vs direct food-contact adhesive and coating claims.
- Request a coating + bond trial kit
Line-side pilot for repulpable barrier and cup adhesive on your facestock—scoped to your food-contact file.
" On the pilot grade, Senda helped us align barrier coat, side seam, and bottom bond so leak screening and our internal recyclability checklist could move forward together—without assuming one adhesive change would fix every forming variable. "
Ready to Write Your Own Success Story?
Our technical engineers are ready to help you solve your specific adhesion challenges. Get in touch for a free consultation and sample testing.
Replicate This Success


