Machine-side guide for poly mailer auto-baggers: application temperature, bead geometry, sub-0.5s set time, clean nozzle cutoff, and destructive bond validation on PCR PE—without inventing line-speed guarantees beyond your equipment rating.
Table of Contents
Auto-bagging lines fail in two languages: the seal looks closed but peels open under pilferage force, or the nozzle throws adhesive and stops the line. Both problems are usually temperature, bead geometry, or maintenance—not “weak glue” alone. Start from our courier bag adhesives page for tamper-evident targets and film structures.
Application Temperature and Viscosity Window
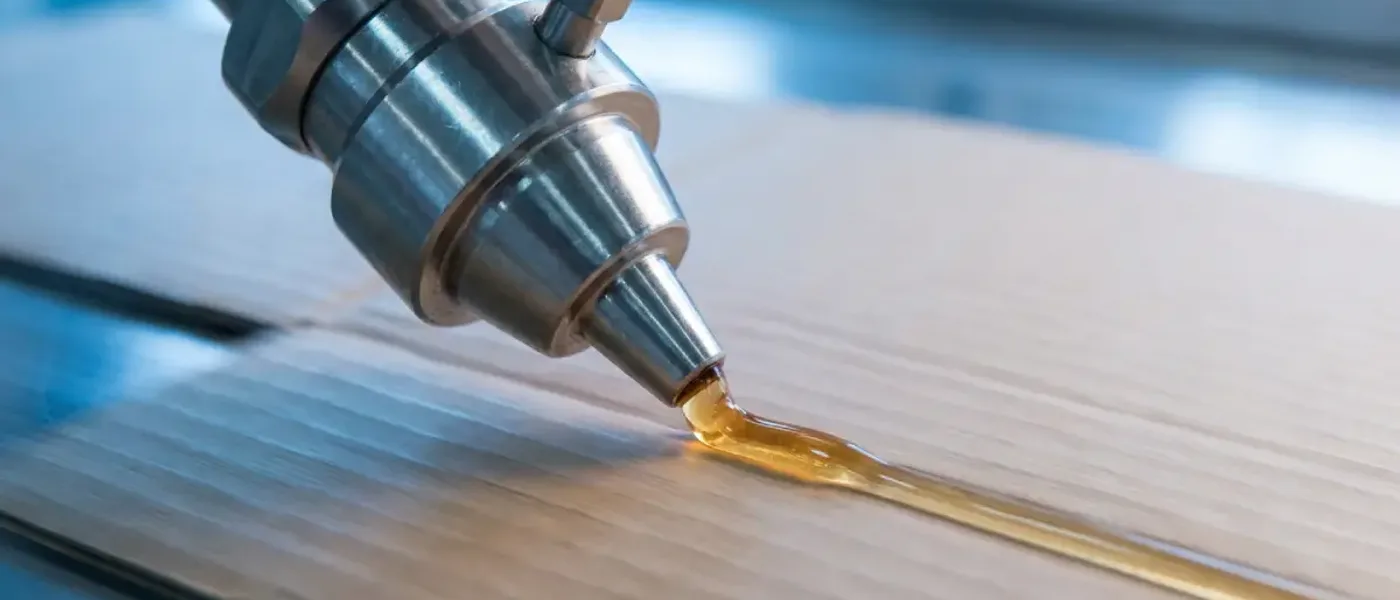
Hot melt on thin PE and co-ex flaps needs fast wet-out without overheating the film. Log tank, hose, and nozzle setpoints at shift start and after film changes. Viscosity that is too low causes misting; too high causes stringing and poor cutoff.
Bead Geometry and Compression
- Bead placement: Center the bead on the flap bond line; offset beads shift peel stress and mimic “weak tack.”
- Compression time: Sub-0.5s set claims on our courier page assume adequate jaw pressure—verify on your thinnest gauge.
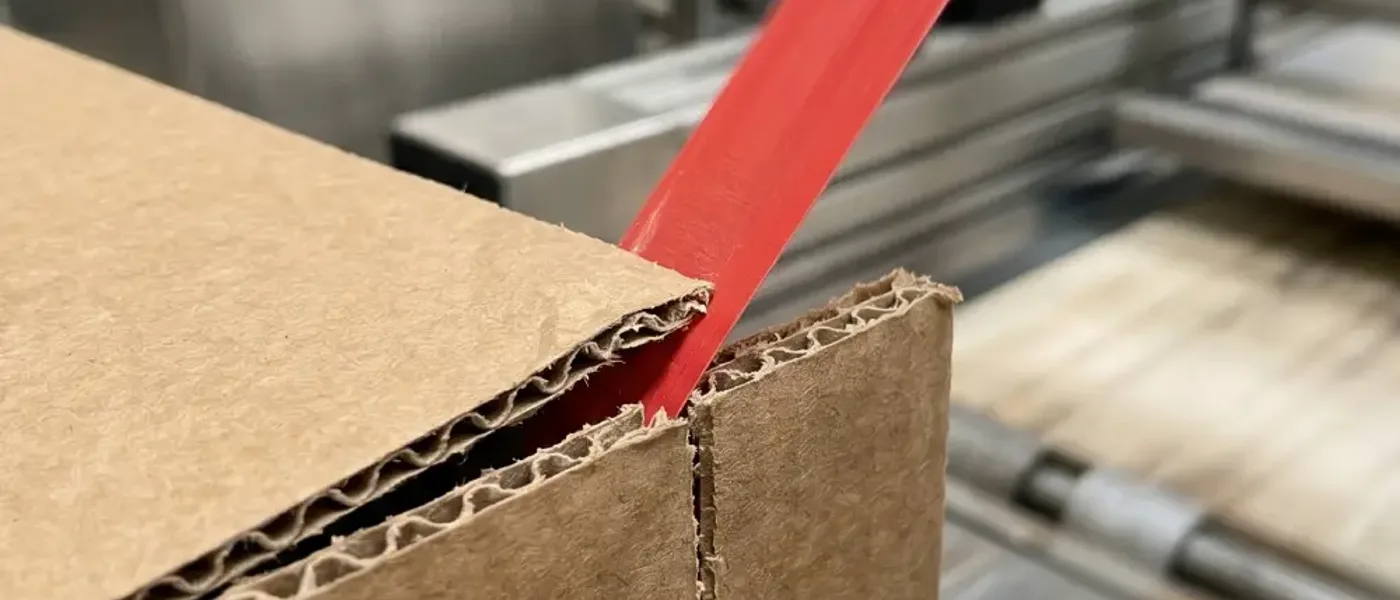
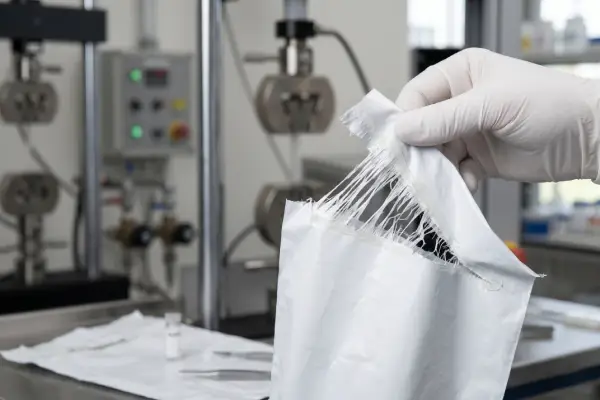
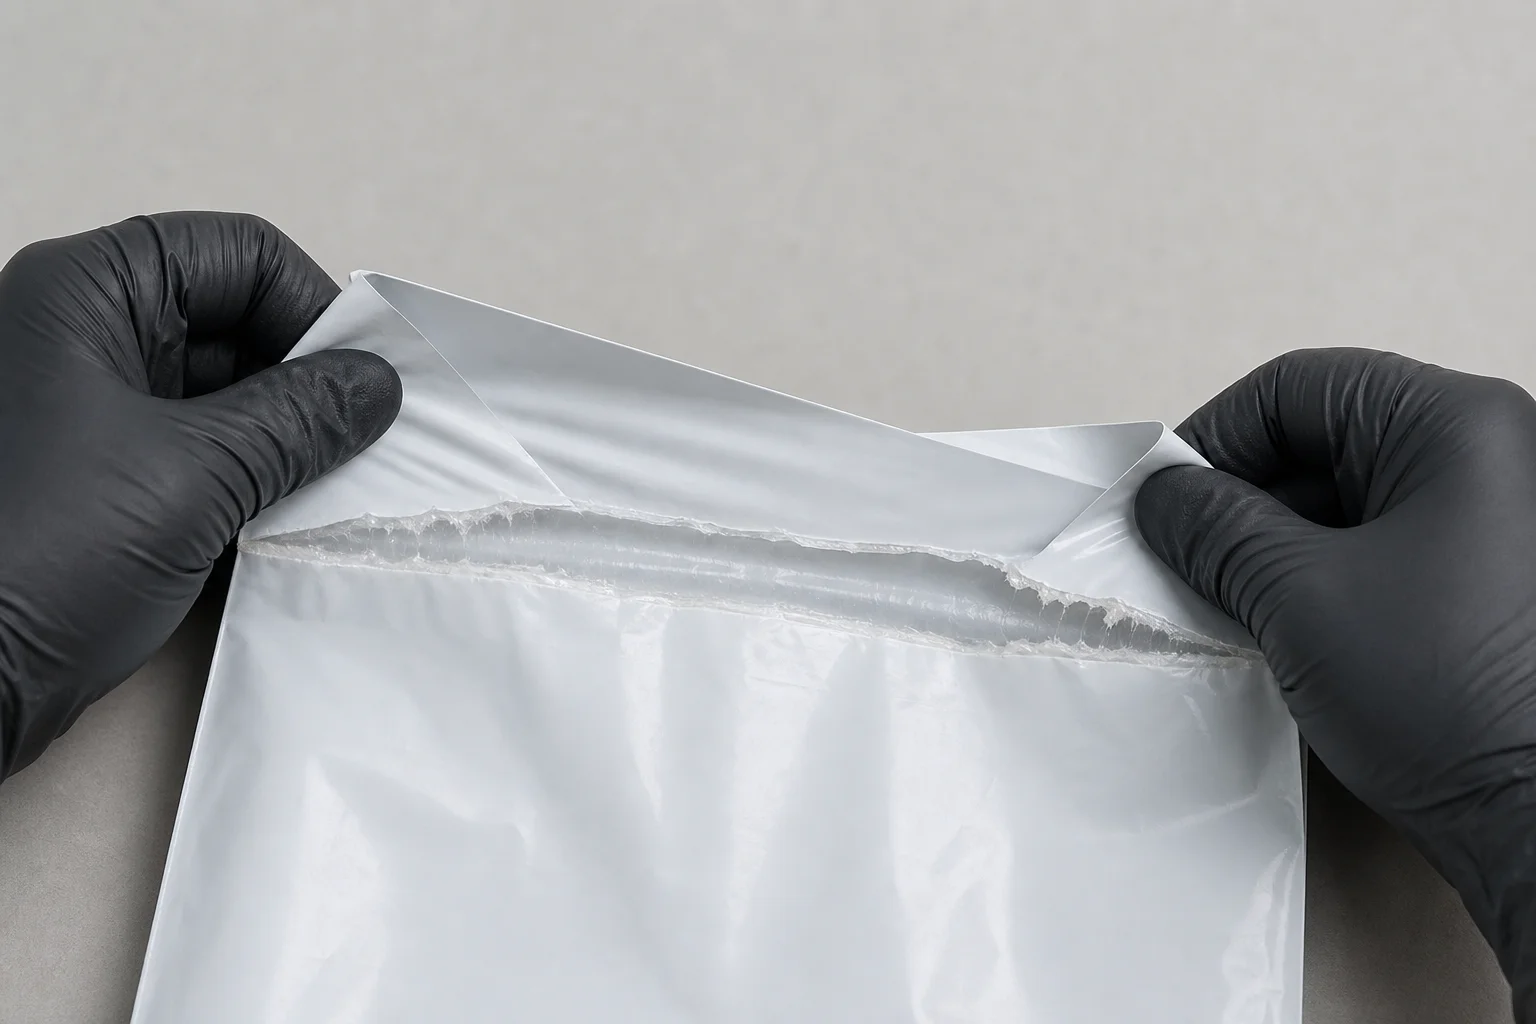
- Destructive bond check: Forced opening should tear film, not lift a clean peel strip—validate against our e-commerce tamper-proof case study.
Peelable Seals Instead of Destructive Bond?
Review courier bag PSA grades for tamper-evident film tear and sub-second seal development on auto-baggers.
See Courier Bag AdhesivesNozzle Maintenance Discipline
- Clean knives, sensors, and sealing jaws on a defined interval.
- Purge on grade change; mixed hot melts often spike stringing on restart.
- Document line speed only after cutoff is stable at that setpoint.
Field Evidence
A fulfillment program replaced peelable closures with Senda PSA and achieved visible film tear on forced opening—e-commerce tamper-proof case study.
Final Takeaway
Optimize temperature and bead geometry before swapping polymer platforms. Destructive bond validation should precede any EVA vs. metallocene trial on the same mailer film.
Frequently Asked Questions
What set time do you target on auto-baggers?
Our courier bag page cites sub-0.5 second green strength for high-speed sealing heads—validate on your film gauge, flap geometry, and compression time; do not assume the same window on every OEM.
Will this work on recycled PCR mailers?
Yes. High-flow grades are positioned for rough PCR polyethylene wet-out and visible film tear on forced opening—always run destructive-open tests on your actual bag lot.
How do I reduce nozzle stringing at 100+ bags/min?
Stabilize temperature inside the grade’s viscosity window, clean knives and jaws on schedule, and avoid mixing incompatible hot melts in the tank before blaming chemistry.
Validate seal window on your bagger
Request complimentary 1 kg lab material (shipping prepaid by recipient) after screening on your substrate and line conditions.
References
Technical Disclaimer: All technical data is based on standard laboratory conditions. Users should perform their own verification testing to confirm suitability for specific substrates, processes, and regulatory requirements. Senda Glue makes no warranties, express or implied, and assumes no liability for improper use of the products or reliance on this information.