
Honeycomb Board Adhesive for Lay-Flat Lamination

Factory-direct paper honeycomb glue and honeycomb board adhesive for pallets, door fill, and structural panels. Low-moisture dextrin/PVA grades for anti-curl lamination and compression targets on your core—1 kg lab screen, then 20 kg trial.
*Complimentary 1 kg lab material · shipping prepaid by recipient. 20 kg pails for laminator trials after screening. MOQ typically ~1,000 kg.*
✅ Lay-flat & compression qualified on your panel • 175.105 routes where packaging applies • Repulpable water-based options (mill-dependent)
Optimized For:
Low-moisture
Solids tuned to reduce curl / banana effect
Compression
Vertical load screened on your core build
Dextrin/PVA
Bio-based starch routes where specified
Honeycomb Programs We Qualify
Pallets, door fill, furniture panels, and buffers need different moisture budgets and compression targets—one honeycomb glue rarely fits every laminator.
Paper Pallets & Dunnage
Structural lamination for export pallets—qualify vertical compression on your cell size and liner GSM, not a generic kg/m² brochure figure.
Door Core Fillers
Moisture-controlled bonds for hollow cores—screen lay-flat geometry after drying, not only wet tack at the press.
Furniture & Flat-Pack Panels
Stiff liner-to-core bonds for lightweight composites—validate delamination under flex and humidity cycling.
Protective Buffer Panels
Shock buffers and void fill—balance impact performance with drying time on high-humidity transit lanes.
From Curl & Delamination to Qualified Panels
Honeycomb defects are usually moisture + bond together—flat panels that fail compression (or strong bonds that warp) both need line-side qualification.
Common Failures
Board Warping (Banana Effect)
Too much moisture in standard glue causes uneven fiber expansion—warped panels fail automatic fill and pallet assembly.
Liner–Core Delamination
Weak internal bonds let cells separate under load—collapsed pallets and structural failures in the field.
Drying Bottlenecks
High water add-on stretches clamp/oven time and forces lines to run below rated capacity.
Our Solution
Low-Moisture Lamination
Higher-solids routes to limit moisture carry—target lay-flat behavior on your paper stack and press conditions.
Liner & Cell Wetting
Wetting and tack tuned for kraft liners and hex cells—internal bond screened under your compression scenario.
Drying-Window Fit
Emulsion break and set speed matched to nip and oven—approve from dry-to-stack trials, not datasheet open time alone.
Lab Support for Honeycomb Lines
We test curl, compression, and drying on your panel build—not fixed marketing guarantees.
Vertical Compression Screening
Load tests aligned to your pallet or panel spec—targets agreed in trial, not a universal kg/m² claim.
Lay-Flat / Anti-Curl Protocol
Geometry checks after conditioned drying—pair with moisture/add-on review on the laminator.
Expansion & Panel Trials
Separate qualification for core expansion vs face lamination stations when both run in your plant.
Tune to Core Process, Panel & Load Target
Expansion, panel lamination, and heavy structural programs use different chemistries—confirm on your equipment.
| Application | Technology | Viscosity (typical) | Engineering benefit |
|---|---|---|---|
| Core expansion / pull-winding | 800–1,500 cps | Bio-based dextrin | Wet tack for cell stability during expansion—speed qualified on your line. |
| Panel lamination (lay-flat) | 2,000–4,000 cps | High-solid PVA | Lower moisture carry to reduce curl on qualified liner/core pairs. |
| Heavy structural loads | 1,500–3,500 cps | Toughened PVA blend | Compression screening for pallet-grade builds on your cell geometry. |
Technology: 800–1,500 cps
Viscosity (typical): Bio-based dextrin
Engineering benefit: Wet tack for cell stability during expansion—speed qualified on your line.
Technology: 2,000–4,000 cps
Viscosity (typical): High-solid PVA
Engineering benefit: Lower moisture carry to reduce curl on qualified liner/core pairs.
Technology: 1,500–3,500 cps
Viscosity (typical): Toughened PVA blend
Engineering benefit: Compression screening for pallet-grade builds on your cell geometry.
Why Honeycomb Converters Shortlist Senda
Lay-flat and compression qualified together, laminator-tuned honeycomb board glue, and audit paperwork—without guaranteed % faster or 100% recyclable blanket claims.
Curl + Compression Together
Moisture-Aware Chemistry
Audit-Ready Documentation
Documentation for Packaging & Export Programs
Structural honeycomb for secondary packaging may need 175.105 statements—confirm end use before you claim food-adjacent compliance.
Compliance Scope (Confirm for Your Program)
Recyclability depends on facings, inks, and mill equipment—not adhesive marketing alone.
- FDA 175.105 ( Indirect food-packaging routes where applicable (structure-dependent) )
- REACH & RoHS ( SVHC statements on request )
- Repulpable routes ( Water-based starch/PVA—mill and stack dependent )
Batch-level TDS, SDS, DoC, and CoA for the nominated grade—scoped to your honeycomb program.
Related Paper Converting Lines
Honeycomb plants often run edge protectors and paper cores on the same site—route each line to the right chemistry.


Curl was killing our door-fill program until we qualified a lower-moisture lamination route. Senda’s panel protocol tied lay-flat checks to compression screening—not just “less glue water” on a slide.
Technical Proof (Optional Reading)
Share with process engineering after you request samples. Primary path: lab screen + audit package via the buttons above.
 CASE STUDY
Case Study: Honeycomb Board Curl Control
How a structural panel converter improved lay-flat output and compression confidence with a lower-moisture lamination system.
Read the Full Story →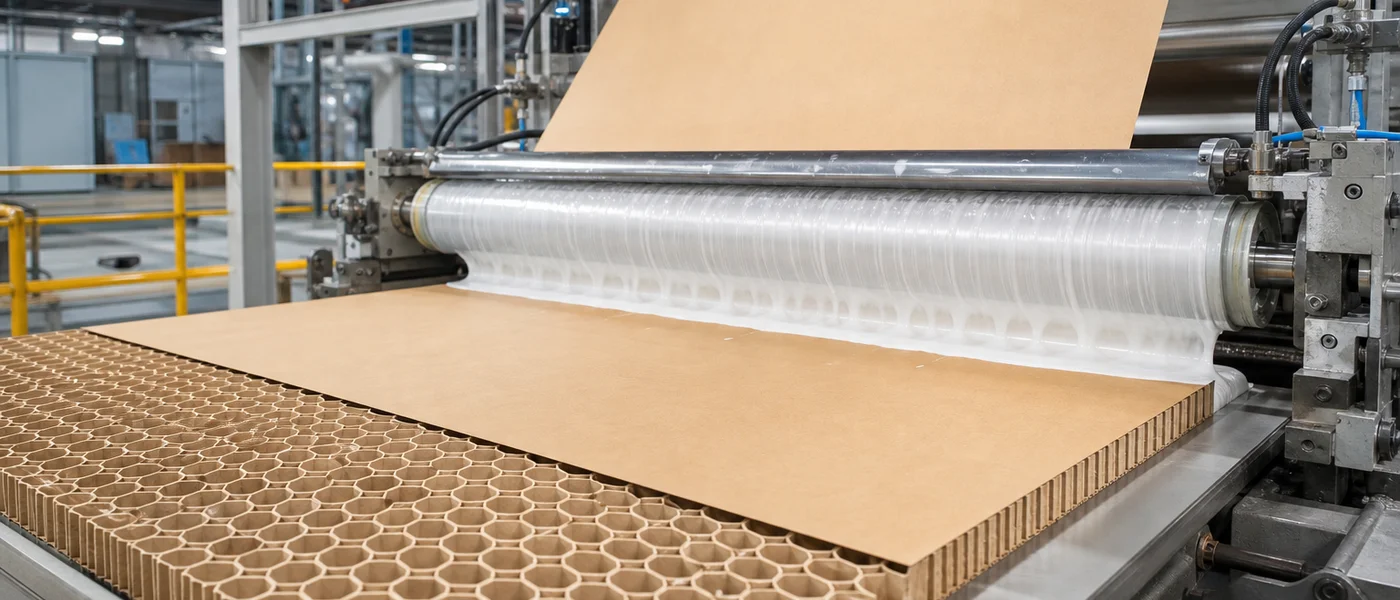 TECHNICAL GUIDE
Guide: Preventing Honeycomb Defects
Moisture, glue spread, nip pressure, and drying balance to limit warping and delamination.
Read Full Article →Frequently Asked Questions
Find answers to common questions about our adhesive solutions and services.
What adhesive is used for honeycomb board lamination?
Most programs use water-based dextrin for core expansion and high-solid PVA for panel lamination—grade choice depends on moisture budget, cell size, and compression targets. Start with a 1 kg sample on your line.
What are MOQ, lead time, and sample options?
MOQ is typically ~1,000 kg. Lead time is often 7–10 business days for qualified grades. Complimentary 1 kg lab material (recipient prepaid shipping), plus 20 kg pails for laminator validation.
How do you prevent honeycomb board curling?
We reduce moisture carry with higher-solids systems and match add-on, nip, and drying to your paper—qualify lay-flat after conditioning, not only at the press exit.
What compression strength can honeycomb panels achieve?
Compression is panel-dependent (cell size, liner GSM, adhesive add-on). We screen your build toward agreed targets—do not assume a universal kg/m² figure from marketing copy.
Are honeycomb adhesives bio-based or repulpable?
Many routes use starch/dextrin feedstocks; repulpability depends on the full panel stack and your mill. Run an internal repulp test on the nominated grade.
Do you meet FDA or REACH requirements?
175.105 may apply to some secondary packaging programs; REACH/RoHS documents are provided on request for nominated grades.
How do moisture, spread rate, and pressure affect defects?
All three interact with chemistry—see the honeycomb defect prevention guide (Resources) before changing only adhesive grade.
What shelf life and storage conditions should we plan for the approved grade?
Typically 6–12 months sealed at about 5–35°C—protect water-based grades from freezing; confirm on the TDS.
